How Custom Football Cleats Are Made: Tech, Costs, and Rules Explained
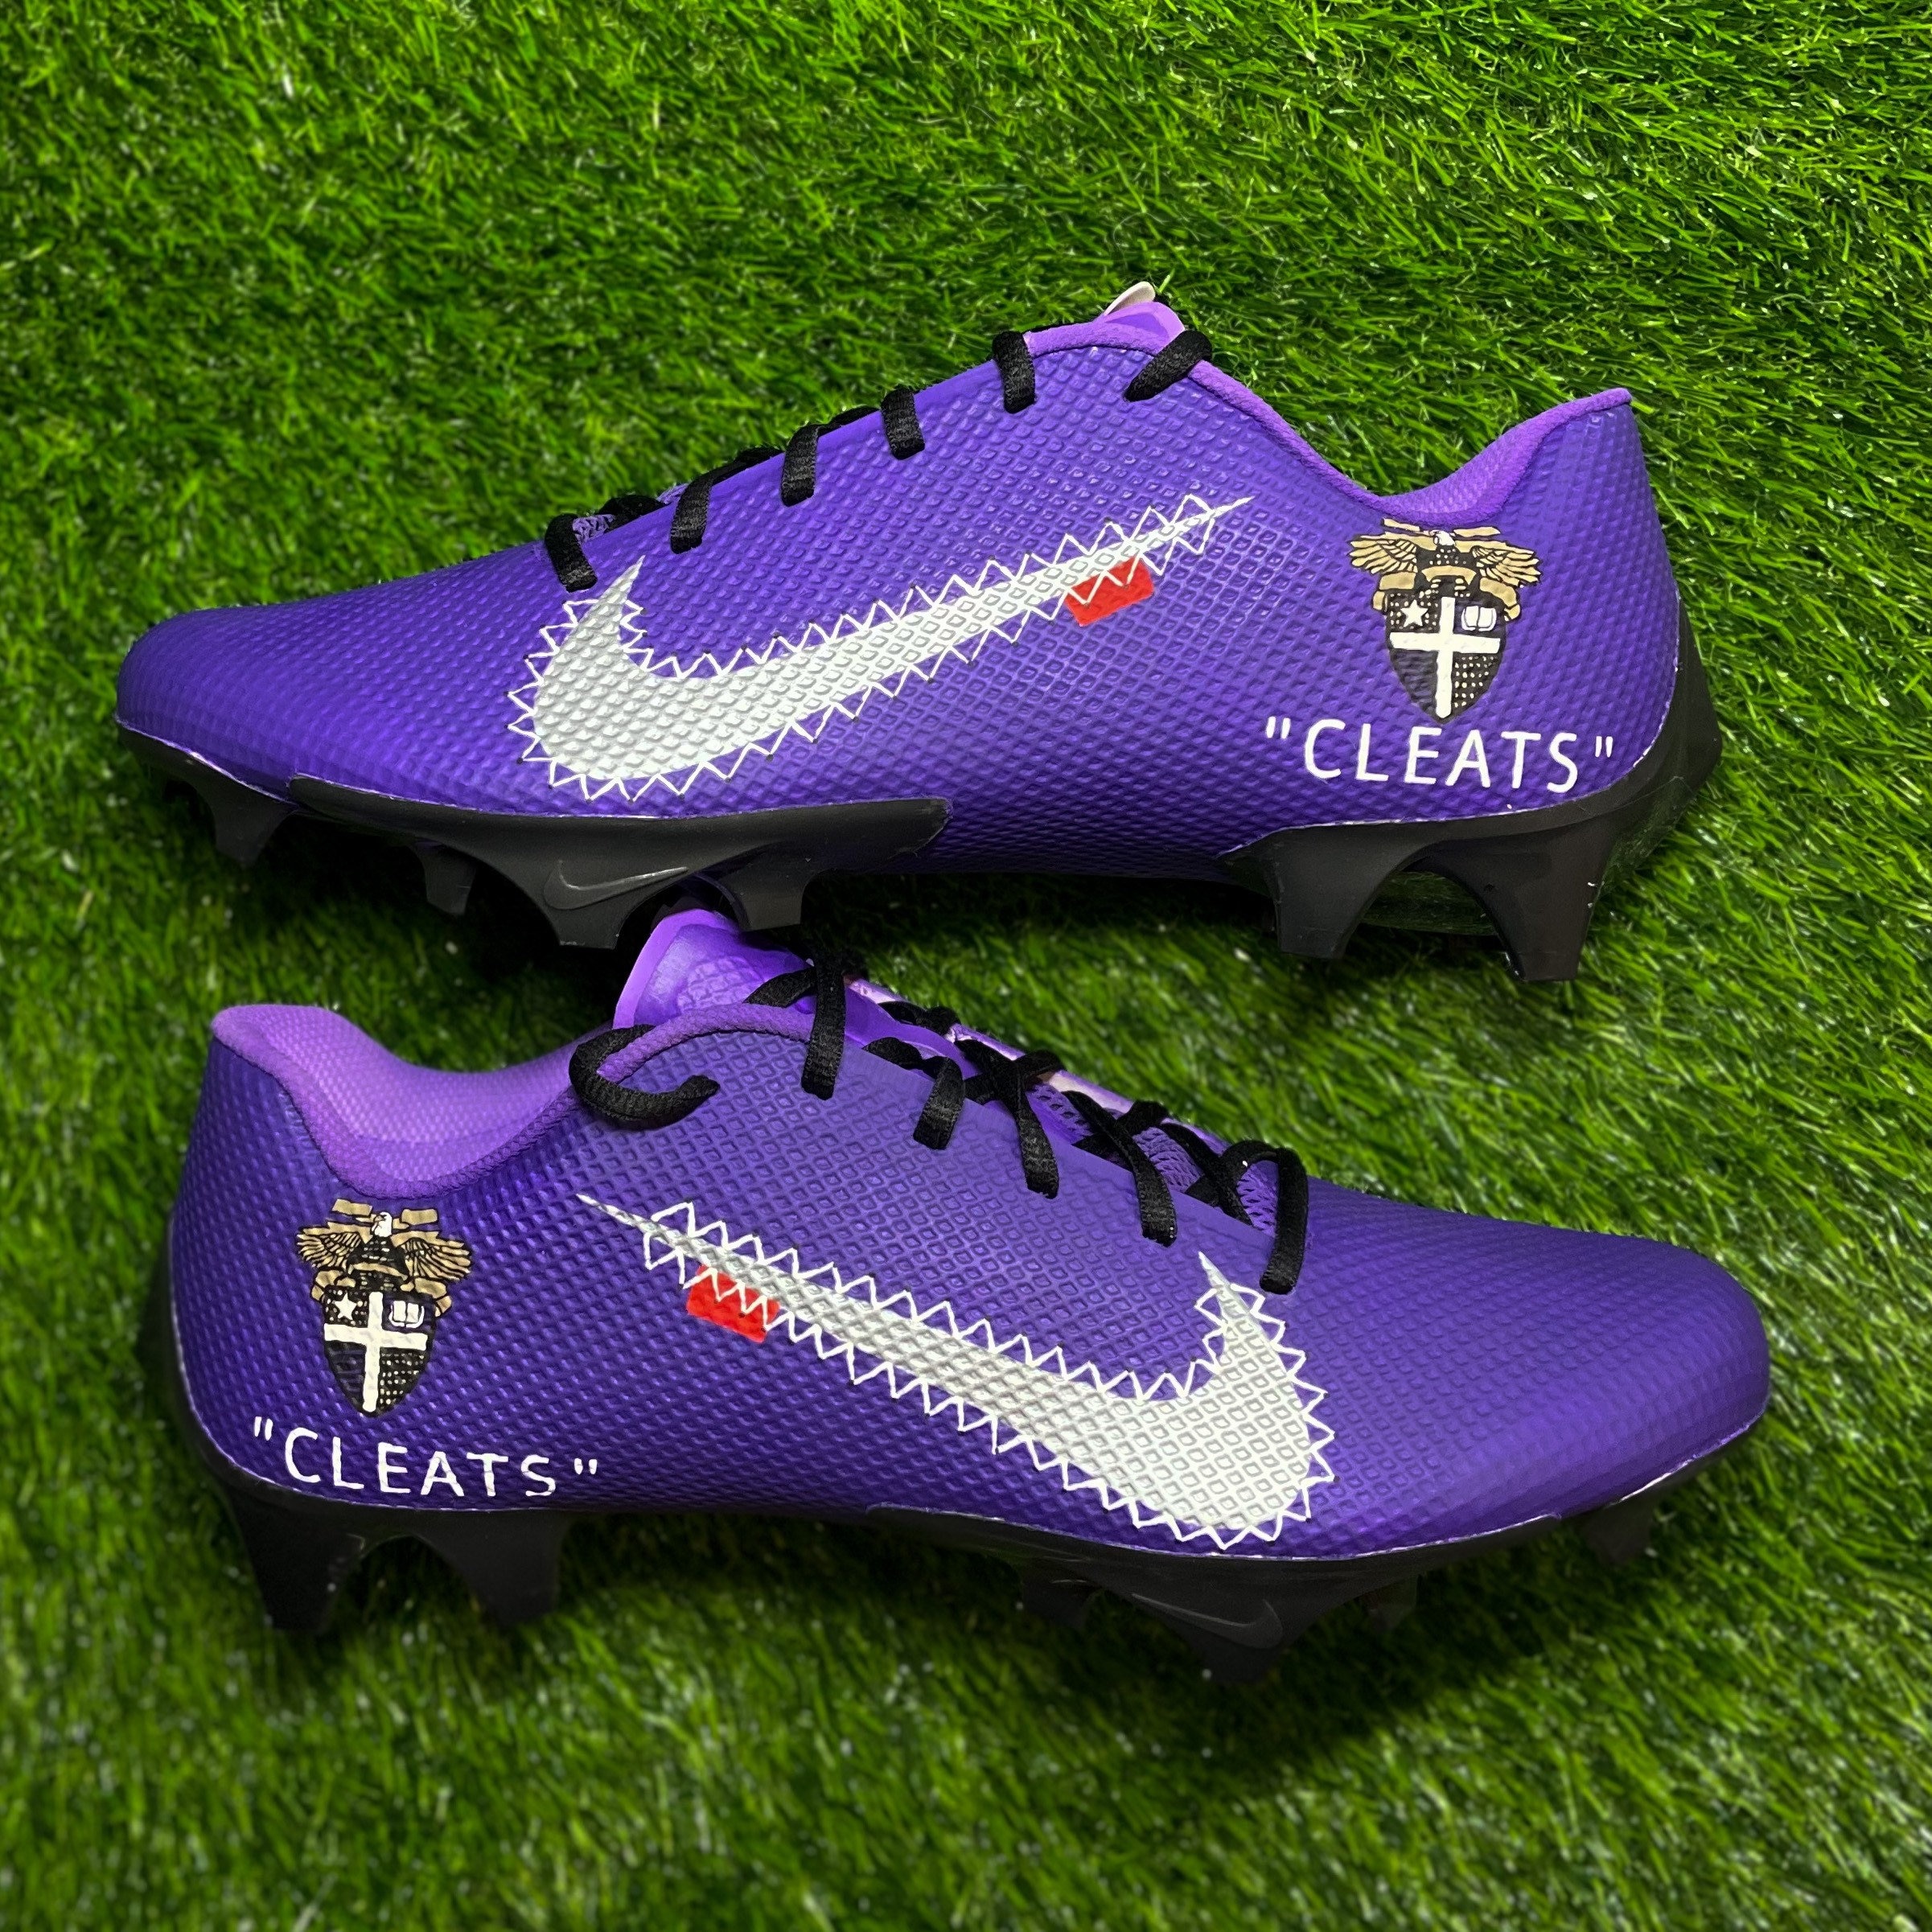
Transforming athletic footwear requires flexible chemistry. The baseline standard across professional studios remains Angelus leather paint, a specialized water-based acrylic emulsion formulated to stretch without micro-fracturing. Artists mix the pigment with leveling agents and flow additives to feed needle-fine airbrush nozzles.
Applying the paint correctly requires compounding for specific textiles:
- Synthetic Leather & Plastics: Technicians blend the pigment with adhesion promoters like Angelus 2-Hard at a 1:1 ratio, heat-curing the layer to lock onto rigid TPU heel counters.
- Knit Collars & Mesh: The color is blended with fabric mediums like 2-Soft at a 1:1 ratio, penetrating deep into the yarn threads before being set with a 300°F heat gun to retain full fabric breathability.
- Midsole Cushions: Specialized elastic dyes are layered in ultra-thin coats, preventing chalky build-up that cracks when EVA foam compresses under a 220-pound athlete.
When intricate marbling or hyper-complex repeating camouflage patterns are required, technicians turn to hydro dip football cleats. The prepared cleat shell is dipped at a strict 30-degree entry angle through a floating polyvinyl alcohol film misted with chemical activator. Because hydro-dip films are vulnerable to turf abrasion, artists immediately seal the transfer beneath dual coats of automotive-grade matte or satin polyurethane clears.
To produce seamless gradients, drop shadows, and portraiture, artists switch to airbrush athletic footwear setups running dual-action gravity-feed guns at 25 to 35 PSI. Applying five to eight paper-thin coats instead of two thick coats ensures the paint bonds as a pliable, skin-tight membrane that flexes naturally across dynamic cut points.